Case · Automotive · Malaysia
Cutting changeover time on a high-mix automotive machining line
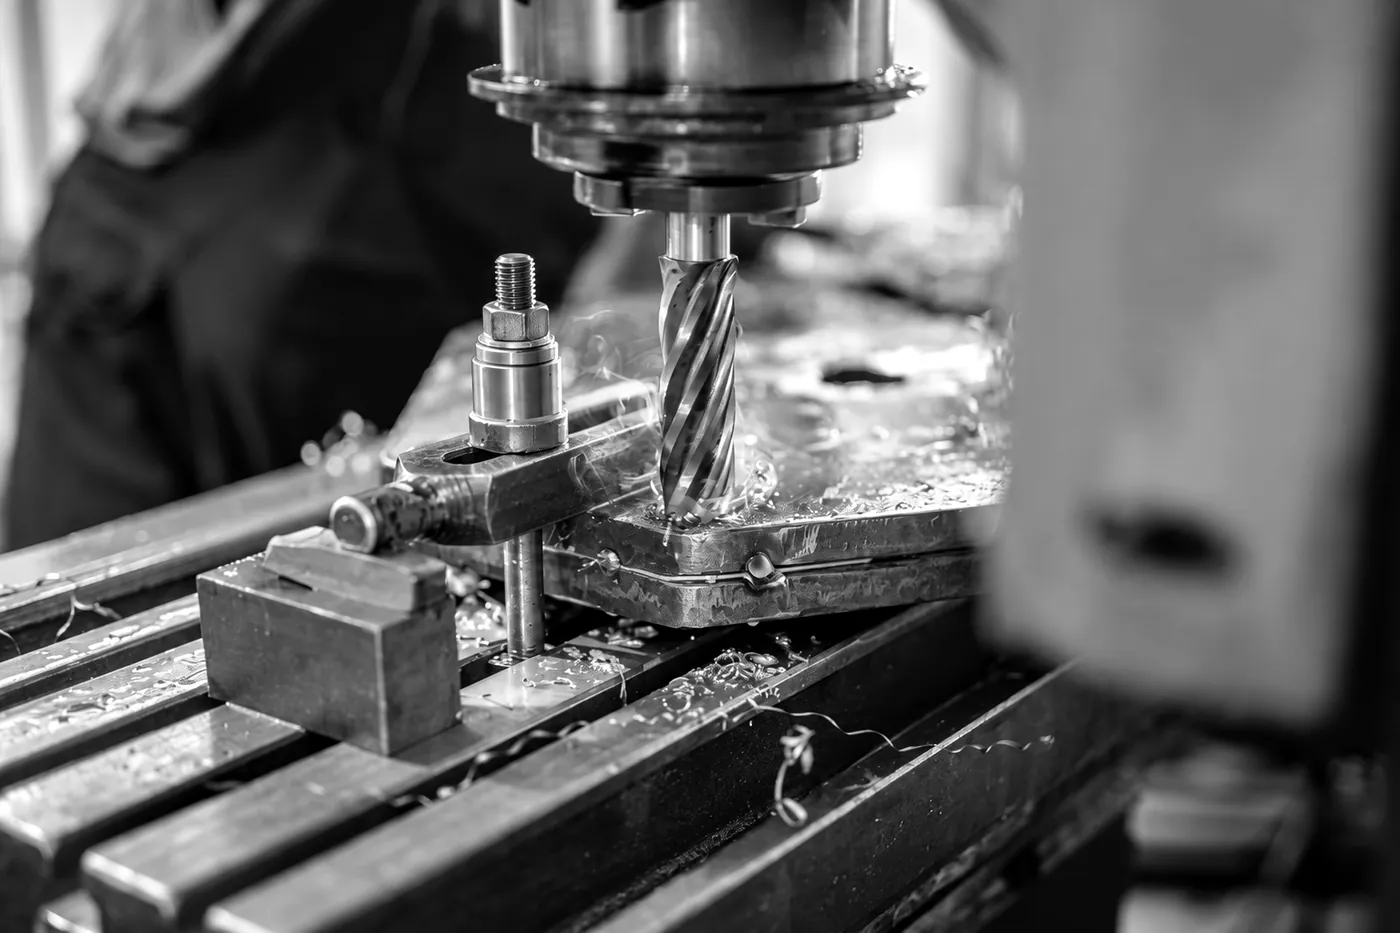
A Tier-2 automotive parts supplier moved its CNC fixtures onto Pitch 96 plates to keep spindles cutting between jobs.
Case at a glance
- Customer
- Automotive parts supplier, Malaysia
- Region
- Malaysia
- Application
- Machining of automotive housings and brackets
- Products used
- Zero-Point Plates, Accessories
01
The challenge
The supplier runs many part numbers in small and medium batches on a bank of machining centres. Each job change meant unbolting, re-clamping and re-indicating the fixture, which kept spindles idle and made first-off results depend on the operator.
The plant wanted a fixture change that any operator could repeat, without giving up rigidity on heavy cuts.
02
The solution
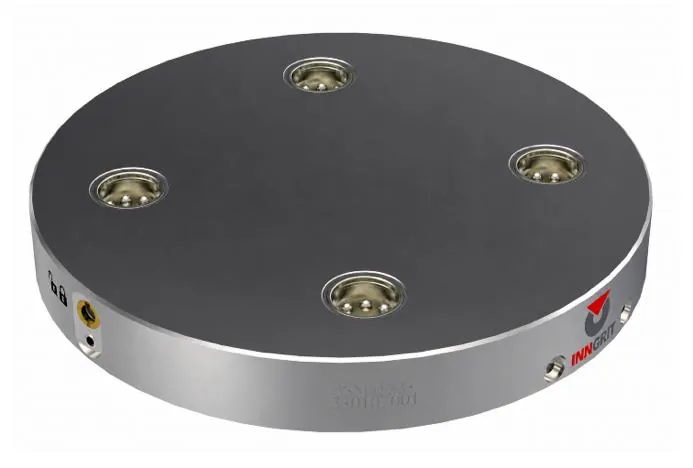
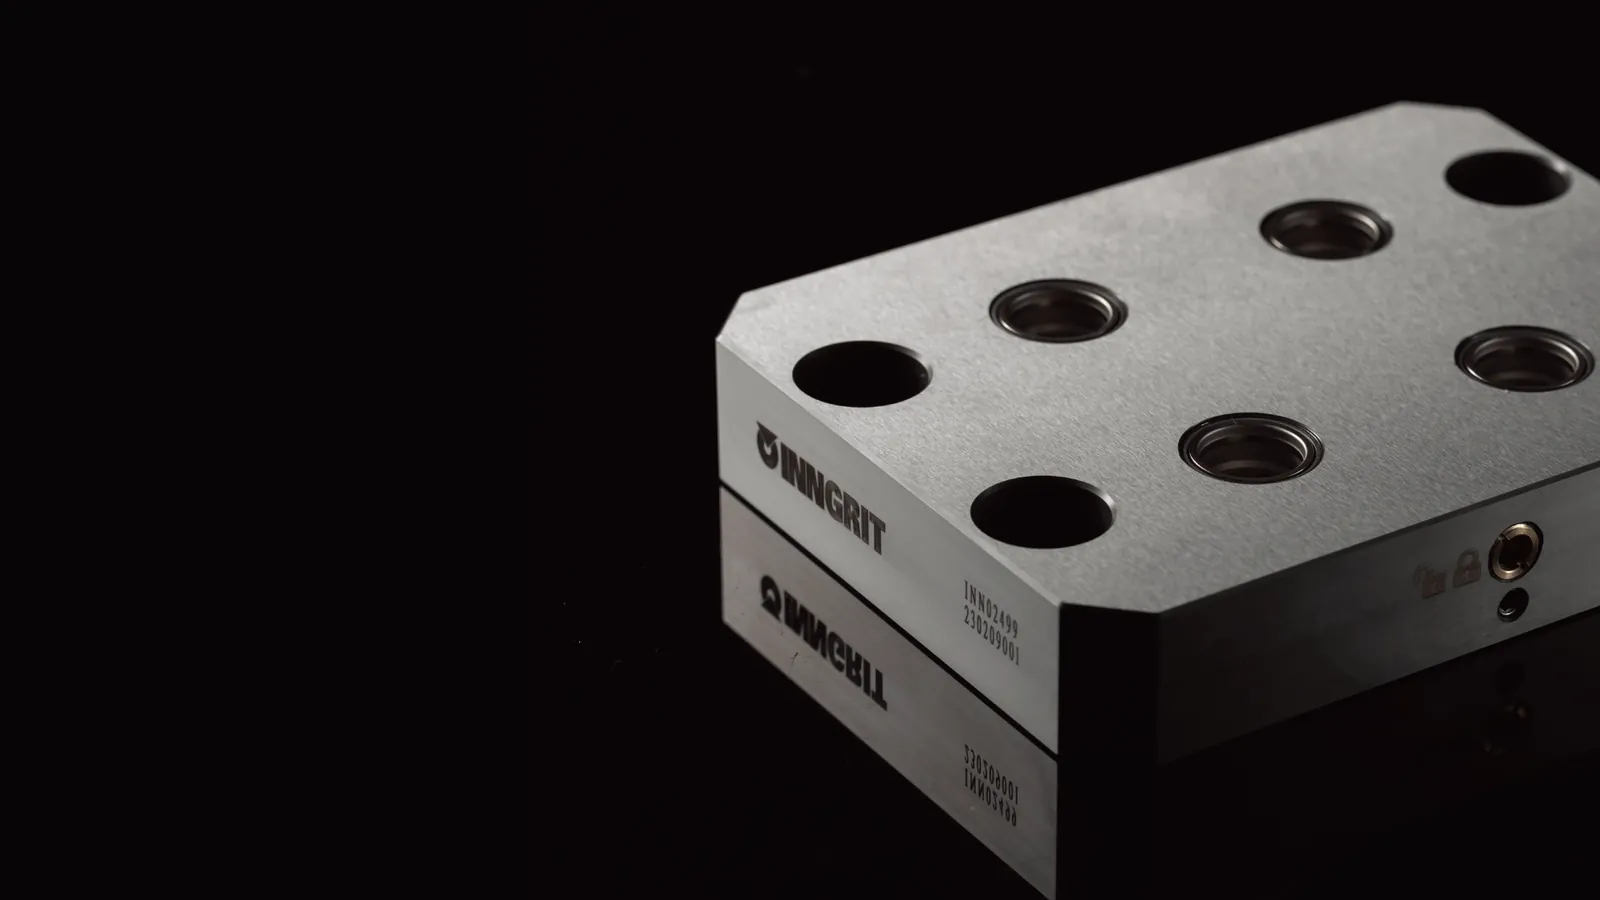
The cell was fitted with Pitch 96 round and square zero-point plates, each 27 mm thick, so fixtures could be changed without lifting the machine table height. Clamping studs HL02727 were torqued to the 20–30 N·m range.
Plates with the patented AIR option were chosen for the cells that run longer, so chips are blown clear before each fixture lands.
03
The results
- Fixture changeover time
- 45 → 8 min
- Changeovers per shift
- 3 → 6
- INNGRIT positioning accuracy specification, unchanged between changes
- Below 0.005 mm
Illustrative figures for this sample case. Results depend on the application.
Customer quote
“We stopped treating a fixture change as a small project. It is now a routine step, and new operators learn it in a shift.”
Related cases
All cases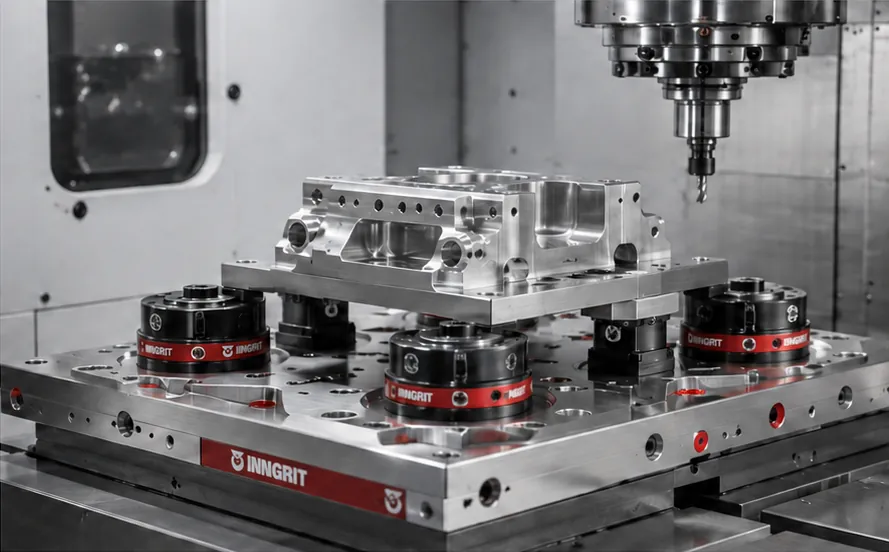
Aerospace / Germany
Repeatable re-clamping for 5-axis aerospace components
An aerospace machining shop standardised multi-face set-ups so parts return to the same datum between operations.
Automation / Taiwan
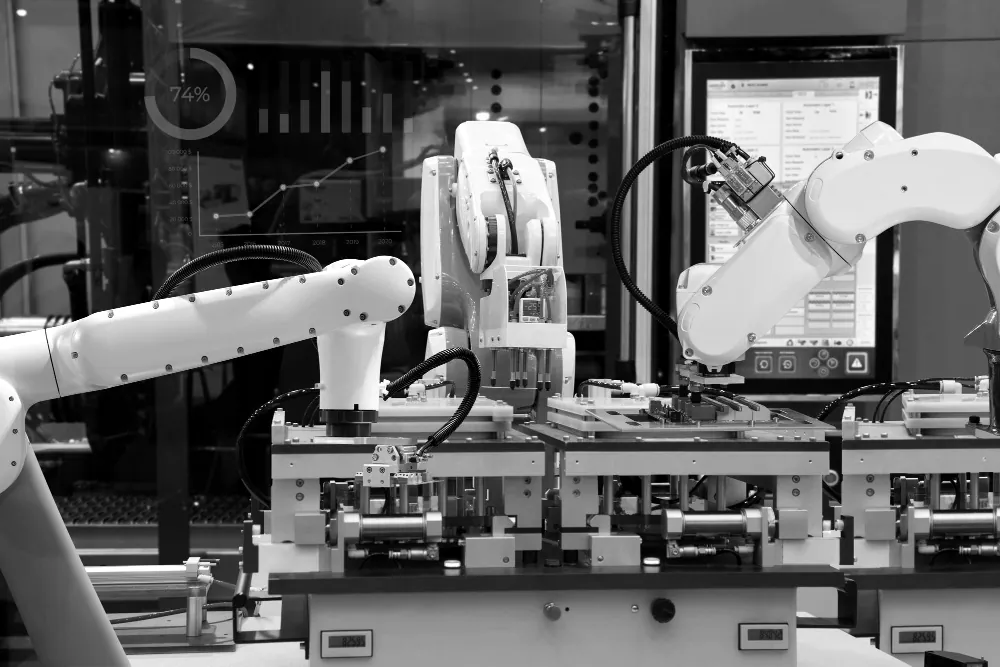
An unattended robot cell that changes its own fixtures
A system integrator built a robot-fed cell where the robot swaps fixtures and grippers on one datum.
Medical / Singapore
Fast, clean changeovers for small-batch medical components
A contract manufacturer moved small-batch medical parts onto compact Pitch 52 plates to cut changeover time.